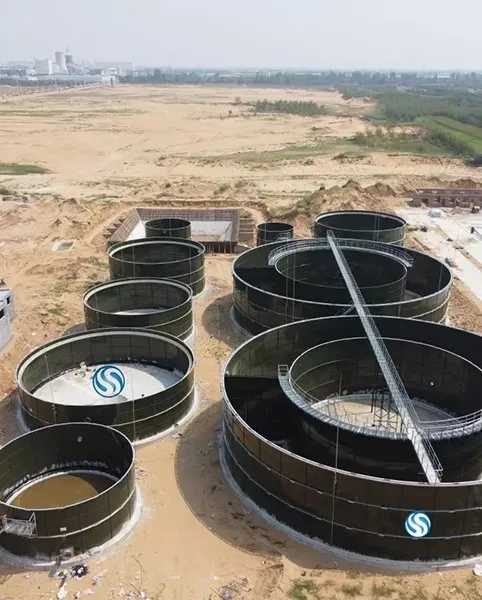
Receiving damaged panels is a common concern when preparing Custom GFS Tanks for assembly. Small chips, scratches, exposed steel, or damaged edges can become corrosion initiation points if they are hidden under a bolt seam or installed before repair. This guide explains how to repair minor GFS panel damage before installation, with practical controls for GFS tank panel repair, repairing chipped glass fused to steel panels, and inspecting Glass Fused to Steel Tanks. The correct approach is not to repaint a panel with ordinary enamel; it is to identify the coating defect, use a manufacturer-approved repair system, verify the cured repair, and document the result before assembly.
For a Wansheng project or any other supplier’s tank, the panel manufacturer’s repair instructions take priority over generic advice. Glass-fused-to-steel panels use a factory-applied enamel coating, and the repair material must be chemically and mechanically compatible with that coating. A repair that looks acceptable but fails holiday detection, has inadequate dry-film thickness, or leaves corrosion under the edge can create a larger installation problem later.

GFS panels combine a steel substrate with a fused glass or porcelain-enamel coating. The steel provides structural strength, while the enamel coating separates the steel from water, oxygen, salts, and biological contaminants. Damage is therefore assessed by depth and location, not only by appearance.
- Surface scuff: The coating is visibly marked, but no steel is exposed.
- Chip or pinhole: A small area of enamel is missing and the substrate may be visible.
- Edge damage: The coating is broken near a panel edge, bolt hole, flange, or joint.
- Corrosion staining: Brown or orange discoloration indicates that moisture may have reached the steel.
- Structural distortion: A bent panel, enlarged bolt hole, cracked flange, or distorted seam is not a minor coating defect and should be quarantined.
Bolted tank panels are especially sensitive at connection zones. A coating defect near a seam can be concealed by a gasket or joint sealant, making later inspection difficult. Repairing the defect before installation allows the inspector to clean the steel properly, apply the approved system under controlled conditions, and confirm the repair before the panel is lifted.
Why Glass Fused to Steel Tanks Need Pre-Installation Repair
Repair decisions should be based on traceable documents rather than an invented anecdote or an unverified online post. The main technical references for this work include the project specification, the GFS supplier’s repair manual, the applicable edition of AWWA D103 where specified for factory-coated bolted steel tanks, and ISO 28765 where vitrified-coated steel tanks are covered by the project. These documents define requirements that can differ by coating system, tank service, and manufacturer.
No private installer story is presented here as a “real case” because an individual site report cannot be verified from the information supplied. Instead, use the following source-controlled inspection case format on the job: record the panel number, damage location, defect size, exposed-substrate condition, repair-product batch, ambient conditions, cure time, inspection result, and inspector’s signature. This produces a verifiable project record rather than an untraceable claim about performance.
Verified Information and Case-Selection Note for GFS Panel Repair
Required Preparation for GFS Tank Panel Repair
Before touching a damaged panel, collect the latest approved documents:
- Panel layout and identification drawing.
- Manufacturer-approved repair procedure.
- Approved repair-kit technical data sheet and safety data sheet.
- Project coating inspection and acceptance criteria.
- Required inspection records and nonconformance report form.
Do not begin if the panel is wet, contaminated with oil, heavily corroded, visibly distorted, or damaged around a structural connection beyond the repair limits stated by the manufacturer. Panels with cracks through the steel, severe flange deformation, elongated bolt holes, or uncertain identity should be isolated and referred to the supplier.
Documents and prerequisites for Glass Fused to Steel Tanks
- Clean, padded inspection table or supports.
- White light and a low-angle inspection lamp.
- Camera or mobile device for before-and-after records.
- Lint-free cloths and the cleaner specified by the repair-kit supplier.
- Non-metallic scraper or soft brush.
- Fine abrasive material only if expressly permitted by the repair procedure.
- Manufacturer-approved primer, repair enamel, or compatible two-component repair coating.
- Clean mixing cups, stirrers, and disposable application tools.
- Calibrated thermometer and hygrometer.
- Wet-film or dry-film thickness equipment when required by the product data sheet.
- Approved low-voltage holiday detector or other test equipment specified by the supplier.
- Personal protective equipment, including gloves, eye protection, and suitable respiratory protection where required by the safety data sheet.
Do not substitute automotive paint, household enamel, silicone, construction adhesive, or unapproved epoxy. A product can adhere to steel and still be unsuitable for immersion, drinking-water contact, wastewater exposure, or long-term compatibility with the original enamel coating.
Tools and materials for repairing chipped glass fused to steel panels
Step-by-Step Method for How to Repair Minor GFS Panel Damage Before Installation
1. Quarantine and identify the damaged GFS panel
Tools: Panel drawing, tags, camera, inspection form, padded supports.
Action: Move the panel to a clean, stable support. Mark its panel number and orientation without writing on the enamel. Photograph the full panel, the defect, and a scale reference. Record whether the defect is on the water side, exterior side, edge, flange, or bolt-hole area.
Parameters: Use the project’s panel identification system and measure the defect length and width in millimetres. Do not estimate a repair limit from appearance alone; compare the defect with the supplier’s written minor-repair criteria.
Check: Confirm that the panel is not bent and that bolt holes, flanges, stiffeners, and edges retain their intended shape.
Failure fix: If distortion, cracking, deep corrosion, or structural damage is found, stop cosmetic repair. Attach a nonconformance tag and request a written disposition from the manufacturer or engineer.
2. Classify the coating defect
Tools: Low-angle lamp, magnifier, clean probe approved for inspection, camera.
Action: Examine the defect under direct and oblique light. Separate superficial transfer marks from missing enamel. Look for exposed steel, red rust, undercut edges, multiple pinholes, and damage extending into a seam or bolt hole.
Parameters: Record the defect type and location rather than using vague terms such as “small” or “minor.” The repair product data sheet and GFS supplier procedure determine allowable defect size, number of repairs, edge distance, and coating build.
Check: A superficial mark should not release powder, reveal steel, or have a loose coating edge. A chip exposing steel requires cleaning and a compatible repair system.
Failure fix: If the defect classification is uncertain, treat it as a coating failure and obtain supplier guidance. Do not cover an unknown defect with sealant.
3. Remove loose enamel and contamination
Tools: Non-metallic scraper, soft brush, approved cleaner, lint-free cloths, PPE.
Action: Remove loose fragments and dust without striking the panel. Clean the surrounding area using only the solvent or detergent named in the approved repair procedure. Wipe until no oil, dust, or residue remains.
Parameters: Keep the prepared area within the repair boundary specified by the product manufacturer. Do not use an aggressive solvent that softens the existing enamel or leaves a residue. Do not use a wire wheel or uncontrolled grinding on the glass coating.
Check: The surface should be dry, clean, and free from loose edges. A clean white cloth should not pick up visible oil or dirt after the final wipe.
Failure fix: If oil remains, repeat cleaning with the approved method. If rust is present, follow the repair-kit procedure for rust removal; if the steel cannot be cleaned without enlarging the defect, stop and refer the panel.
4. Prepare the exposed steel or coating edge
Tools: Approved abrasive pad or abrasive paper, vacuum or clean brush, inspection lamp.
Action: Feather only the loose or sharp coating edge if the supplier permits it. Remove corrosion products from exposed steel using the specified preparation method. Vacuum or brush away particles and clean again.
Parameters: Follow the repair product’s surface-preparation grade and do not polish the steel to a glossy surface if the primer requires a keyed profile. Do not increase the repair area merely to make it look symmetrical.
Check: The remaining enamel must be firmly attached, and exposed steel must show no active rust, scale, moisture, or abrasive residue.
Failure fix: If the edge continues to lift during preparation, the defect is larger than initially recorded. Reclassify it and obtain approval before coating.
5. Confirm environmental conditions before applying the repair coating
Tools: Calibrated thermometer, hygrometer, surface-temperature measurement device, product data sheet.
Action: Measure air temperature, relative humidity, and panel temperature immediately before application. Check the product’s recoat, application, and curing limits.
Parameters: Use the exact limits printed in the approved repair product data sheet. Many coating failures are caused by condensation, excessive humidity, or application outside the permitted temperature range. The steel surface must remain above the product’s stated dew-point margin; use the project specification if it gives a stricter requirement.
Check: Confirm that the panel is dry and that conditions are expected to remain within limits throughout the initial cure period.
Failure fix: If conditions are outside the stated range, move the work indoors or control the environment. Do not add thinner or accelerate curing unless the product manufacturer expressly permits it.
6. Mix and apply the approved GFS panel repair material
Tools: Repair kit, mixing cup, calibrated scale where required, stirrer, small brush or applicator, timer, PPE.
Action: Check the product name, batch number, shelf life, and mixing ratio. Mix only the quantity that can be applied within the product’s pot life. Apply the approved primer where required, followed by the compatible repair enamel or topcoat.
Parameters: Use the manufacturer’s specified mixing ratio, induction time, pot life, wet-film thickness, number of coats, and recoat interval. Do not rely on colour matching as proof of correct thickness or chemical compatibility.
Check: The repair should cover the exposed substrate and overlap sound coating without visible pinholes, craters, runs, lifting, or uncoated edges. Record application time and batch details.
Failure fix: If the coating sags, wrinkles, separates, or develops pinholes, do not touch it while partially cured. Follow the product’s rework instruction, which may require removal and reapplication.
7. Cure the repair before handling the panel
Tools: Timer, environmental log, protective cover, product data sheet.
Action: Protect the repair from dust, rain, condensation, impact, and lifting equipment. Leave the panel undisturbed for the full cure or handling time stated by the repair product.
Parameters: Cure time depends on chemistry and temperature; never replace the specified time with a general “overnight” rule. A coating may be dry to touch while remaining below its service cure.
Check: Confirm that the surface is firm and that the product’s stated handling condition has been reached. Record actual temperature and humidity during curing.
Failure fix: If the coating remains soft, tacky, or easily marked, extend the cure under approved conditions and investigate mixing ratio, temperature, humidity, and product age before releasing the panel.
8. Inspect and test the repaired area
Tools: Inspection lamp, camera, thickness gauge if specified, calibrated holiday detector if specified, inspection form.
Action: Perform visual inspection first. Measure coating thickness when required by the repair system. Conduct holiday detection only with the voltage, electrode, wetting method, and cure condition specified by the GFS supplier or coating manufacturer.
Parameters: Do not select a test voltage from a generic internet recommendation. Excessive voltage can damage a thin or incompletely cured repair, while an unsuitable method can miss a discontinuity. Use calibrated equipment and record the instrument identification.
Check: The repaired area must meet the approved visual, thickness, adhesion, and holiday-detection criteria. Compare the result with the acceptance requirements, not with personal judgment.
Failure fix: Mark failed locations, determine whether the failure is a pinhole, insufficient coverage, poor adhesion, or incomplete cure, and repair only after the cause is understood. Retest after the required cure period.
9. Release the panel for installation
Tools: Release checklist, repair record, padded lifting accessories, approved storage supports.
Action: Sign off the panel only after inspection records are complete. Use padded supports and prevent repaired faces from contacting steel racks, chains, gravel, or unprotected forks.
Parameters: Maintain the supplier’s storage and handling clearances. Keep repaired surfaces away from standing water and condensation until installation.
Check: Confirm that the panel number, repair location, material batch, cure status, inspection result, and release signature are recorded.
Failure fix: If new damage occurs after repair, return the panel to quarantine and repeat the inspection process. Do not assume that a second scratch is harmless because the first repair passed.
Common Errors in GFS Tank Panel Repair and Their Solutions
Using ordinary paint on a glass fused to steel panel
Ordinary paint may have different adhesion, water resistance, chemical resistance, and service-cure characteristics. Use only the repair system approved for the original coating and tank service.
Painting over rust or moisture
Coating over active corrosion traps contaminants and can cause early blistering or delamination. Remove corrosion according to the approved procedure and verify dryness before application.
Grinding the enamel aggressively
Uncontrolled grinding can enlarge the defect and remove sound coating. Use the least aggressive preparation method that achieves the approved surface condition.
Ignoring edge and bolt-hole damage
Edges and bolt holes experience handling and connection stresses. Inspect them separately and follow the manufacturer’s limits for repairability. Structural deformation is not a touch-up issue.
Skipping holiday detection
A repair can look continuous while containing a pinhole. Where the project or supplier requires holiday detection, perform it with calibrated equipment and approved settings after the repair has cured.
Handling the panel before full cure
Slings, gloves, racks, and adjacent panels can imprint or remove an uncured repair. Use the product’s handling-cure requirement rather than a visual dry-to-touch check.
Failing to record the repair
Without a record, installers may not know where a repair was made or whether it passed inspection. A panel-level repair log improves traceability during assembly, leak testing, and future maintenance.
When Minor GFS Panel Damage Requires Replacement or Engineering Review
Do not repair the panel in the field or workshop as a minor defect when any of the following conditions apply:
- The steel substrate is cracked, perforated, deeply pitted, or severely corroded.
- A flange, stiffener, bolt hole, or panel edge is bent or dimensionally altered.
- The defect extends through a large area or includes widespread delamination.
- The damage is inside a critical seam and the approved repair method does not cover that location.
- The panel has been exposed to chemicals that may have changed the enamel or steel condition.
- The product approval, drinking-water requirement, or project specification prohibits the proposed repair material.
In these situations, request a written repair or replacement decision from the GFS manufacturer, project engineer, or authorized inspector. A replacement decision made before installation is usually easier to control than a concealed defect discovered after the tank has been assembled.
Inspection Checklist for Custom GFS Tanks Before Installation
- Panel identity and orientation confirmed.
- Damage photographed and measured.
- Defect classified as cosmetic, coating-related, edge-related, or structural.
- Approved repair product and procedure verified.
- Surface cleaned and prepared according to the procedure.
- Temperature, humidity, and panel condition recorded.
- Mixing ratio, batch number, pot life, and application time recorded.
- Specified coating thickness and cure time achieved.
- Visual inspection completed.
- Holiday detection, adhesion testing, or other required tests passed.
- Panel protected during storage and released for installation.
Summary and Practical Recommendations for GFS Tank Panel Repair
The safest method for how to repair minor GFS panel damage before installation is controlled and traceable: isolate the panel, identify the defect, clean it without enlarging the damage, apply the manufacturer-approved repair system under recorded conditions, allow the specified cure, and complete the required inspection. For Custom GFS Tanks, Wansheng or another supplier, the supplier’s repair limits and coating data sheet should control the final decision. Careful GFS tank panel repair protects the enamel coating, preserves the integrity of bolted tank panels, and reduces the risk of discovering an unverified defect after assembly. The final acceptance should be supported by visual inspection, documented dry-film thickness where required, and calibrated holiday detection when specified for repairing chipped glass fused to steel panels.